
Sublimation printing on cotton does not work directly: disperse ink bonds only with polyester, so untreated cotton prints fade within the first few washes. Four workarounds exist, from sublimation-ready HTV holding 95% color after 30 washes to coating spray at 85%. This guide covers when each earns its cost, and why DTF usually beats them all for cotton production.
Key Takeaways
- Sublimation ink turns into gas at 200°C and bonds only with polyester; cotton fiber offers zero chemical receptor, so untreated cotton prints wash out fast.
- The four working methods are sublimation-compatible HTV, glitter HTV, polyester coating spray, and DTF film, each adding the missing polyester layer first.
- Wash durability differs by method: HTV-based transfers hold about 95% color after 30 washes, coating spray around 85%, untreated cotton near zero.
- Fabric blends follow a ratio rule: 60%+ polyester sublimates well, 50/50 blends print muted, and 100% cotton requires a workaround layer.
- For shops producing cotton apparel at volume, DTF at 160°C for 15 seconds skips the polyester problem entirely and holds grade 4-5 color fastness across 50+ washes.
Why Sublimation Ink Fails on Cotton
Sublimation printing works through chemistry, not adhesion. At around 200°C, disperse dye particles turn from solid directly into gas and bond with polyester’s hydrophobic polymer chains as the fibers cool, becoming part of the material rather than a layer on it. Cotton fiber is cellulose, a hydrophilic polymer with no receptor sites for disperse dye, so the gas passes over it and recondenses without bonding anything; the visible result looks fine for a wear or two, then launders out because nothing ever attached.
That chemistry also explains why the failure is total rather than gradual: a print on 100% cotton loses most density in the first 5-10 washes because the dye sits as loose particulate on the fiber surface, and by wash 30 nothing remains. The honest framing for customers is that sublimation on untreated cotton is a different process that happens to look similar for a week.
The honest truth about this failure mode: it is total, not gradual, and that is actually useful information. Understanding the mechanism makes every workaround obvious. If the ink needs polyester, you add polyester, and the four working methods below differ only in how and at what cost that polyester layer arrives.
Four Ways to Sublimate on Cotton That Actually Work
Each workaround manufactures the missing polyester surface before the ink arrives, and they differ in durability, cost, and skill required. Independent testing reported by HTVRont puts sublimation HTV at roughly 95% color retention after 30 washes and coating spray at about 85%, while DTF skips sublimation chemistry entirely and holds grade 4-5 color fastness across 50+ machine washes.
| Method | How it works | Wash durability | Relative cost | Skill needed |
|---|---|---|---|---|
| Sublimation HTV | print onto receptive HTV, weed, press onto cotton | ~95% color at 30 washes | medium | weeding + layering |
| Glitter HTV | same, with sparkle surface | high, texture-dependent | medium-high | weeding |
| Coating spray | spray polymer layer, dry, sublimate | ~85% at 30 washes | lowest | even application |
| DTF film + powder | print, powder, cure, press at 160°C/15s | grade 4-5, 50+ washes | medium | standard DTF workflow |
Method choice tracks order profile. Most small shops will get the best result from sublimation HTV on craft orders and should treat spray as a prototype tool. One-off cotton tees with full-color art suit sublimation HTV when a shop already owns a sublimation printer and wants the softest result; craft-scale sellers favor coating spray for its pennies-per-shirt cost and accept the 85% durability; and anything past prototype volume moves to DTF, because the film workflow prices per print instead of per pretreatment step. Based on data from our customers across 50+ countries, shops that start with spray almost always migrate to DTF within a quarter, since pretreating each shirt by hand is the bottleneck that does not scale.
Blended Fabrics: The 60% Polyester Rule
Between the two extremes sits the blend territory where most commercial apparel actually lives, and the sublimation outcome scales directly with polyester percentage. A 65/35 poly-cotton tee sublimates with good color density and slight vintage softening, a 50/50 blend prints noticeably muted because half the fiber accepts nothing, and anything under about 40% polyester produces results too faint to sell. The working threshold we and most production shops use is 60% polyester and above for full-density sublimation, with light-colored garments only, because sublimation white is transparent and dark fabrics offer no white base.
| Fabric | Sublimation result | Density | Verdict |
|---|---|---|---|
| 100% polyester | full chemical bond | 100% | ideal |
| 65/35 poly-cotton | strong bond, soft hand | high, slightly muted | production-ready |
| 50/50 blend | partial bond | visibly muted | acceptable for vintage looks |
| under 40% poly | weak bond | faint | not sellable |
| 100% cotton | no bond | fades in 5-10 washes | needs workaround layer |
Color adds a second constraint on top of ratio. Because sublimation dye is additive and transparent, it only shows true on white or light pastel garments; on heather gray the colors dull, and on any dark fabric the design practically disappears. Blends therefore need both boxes checked, enough polyester to bond and enough base lightness to show color, and when a customer order fails one of the two, DTF or HTV becomes the honest recommendation rather than a heroic sublimation attempt. We recommend testing a swatch of any unfamiliar blend at 200°C for 45-60 seconds before quoting, because blend percentages on care labels are approximate.
The Honest Alternative: DTF for Cotton Production
DTF solves the cotton problem by removing the chemistry requirement altogether. The design prints onto PET film with textile ink, hot-melt powder bonds it mechanically, and a 160°C press for 15 seconds laminates it onto any fiber composition, 100% cotton included, with cold peel finishing. Durability on cotton reaches grade 4-5 color fastness across 50+ machine washes, the hand feel stays flexible because the cured ink layer stretches with the knit, and dark garments work natively since DTF prints its own white underbase instead of relying on transparent dye.
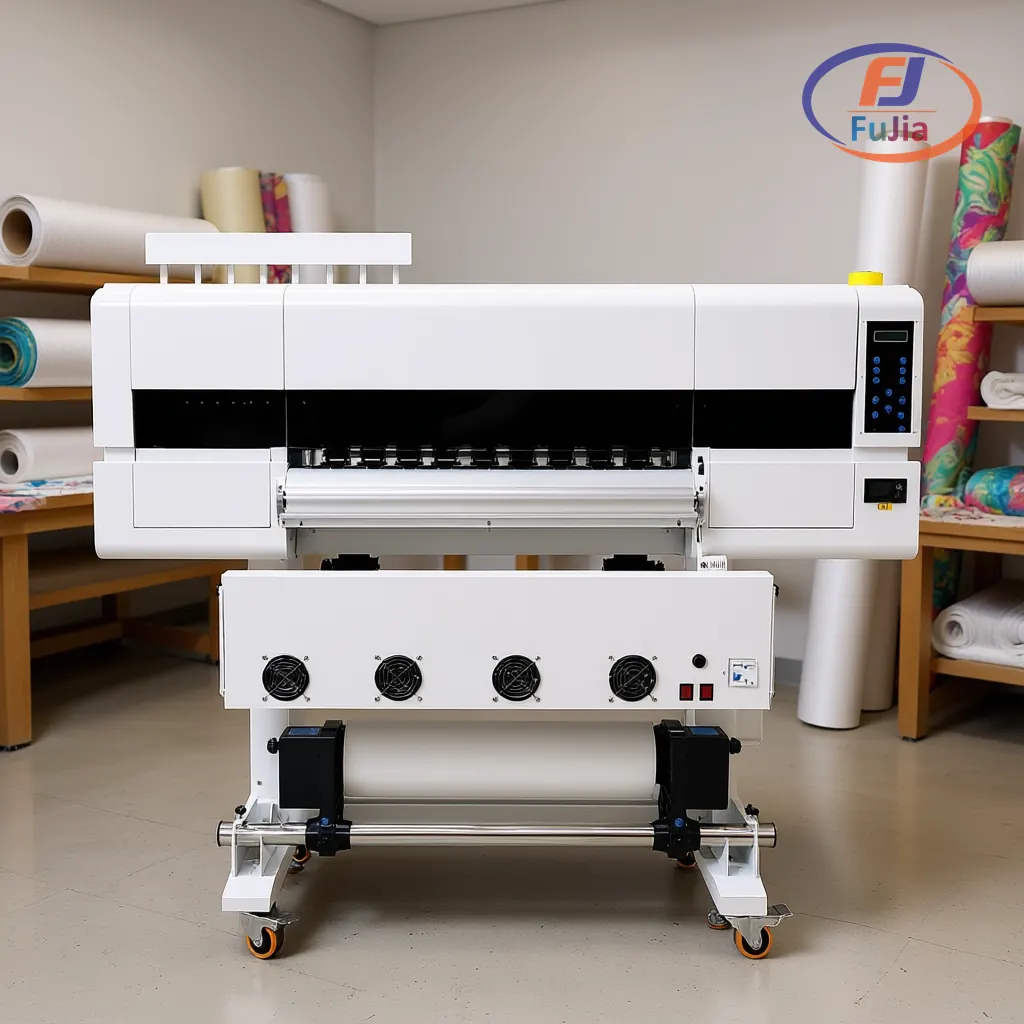
Sublimation keeps real advantages where its chemistry works: a sports bag brand we supplied moved to a 60 cm sublimation printer with a roll heat press for full-bleed edge-to-edge printing on polyester fabric, doubled order value, and has logged zero peeling warranty claims since, and full-width polyester runs are exactly where sublimation beats DTF on speed and per-square-meter cost. The decision line is material, not preference: polyester production favors sublimation, cotton production favors DTF, and blends sit between with the ratio table above as the arbiter.
Based on data from our customers across 50+ countries, shops fielding regular cotton requests add DTF within the first year rather than keep pretreating by hand. Adding an entry DTF printer costs less than losing those orders, and the two workflows share the heat press; the printer, ink, and film differ. Our DTF vs sublimation comparison walks through the full decision, and production-scale options live on the sublimation printers page for the polyester side of the shop.
Can a sublimation printer print on cotton?
Not directly. A sublimation printer fires disperse dye gas that bonds only with polyester fibers, and cotton cellulose offers no receptor, so designs on untreated cotton fade almost completely within 5-10 washes. Four workarounds produce real results: sublimation-compatible HTV holding about 95% color after 30 washes, glitter HTV with a receptive sparkle surface, polyester coating spray at roughly 85% retention, and DTF film with powder, which bypasses sublimation chemistry and holds grade 4-5 fastness across 50+ washes. For mixed-fabric shops the practical answer is both machines: sublimation for polyester production and DTF for cotton work, sharing one heat press between them.
Can I sublimate onto 100% cotton?
Only with a workaround layer, never directly. On 100% cotton the dye has nothing to bond with, so the direct-print result is effectively zero durability, and no press setting changes that chemistry. The two layered options that genuinely work are sublimation HTV, which puts a receptive polyester film between ink and cotton and holds about 95% color after 30 washes, and DTF, which replaces the sublimation step with powder-bonded textile ink at 160°C for 15 seconds. Coating spray also works at roughly 85% retention but adds a pretreatment step per shirt that does not scale. For ongoing 100% cotton production, DTF is the honest recommendation on durability, hand feel, and cost per print.
Can you sublimate on cotton fabric?
Cotton fabric accepts sublimation only after a polyester surface is added, and fabric blends follow a percentage rule. At 65/35 poly-cotton the result is production-ready with high density and a soft vintage hand; at 50/50 the print is visibly muted because half the fibers accept no dye; below about 40% polyester the result is too faint to sell. The full-density threshold is 60% polyester and above on white or light-colored fabric, since sublimation dye is transparent and dark bases leave no visible image. Test pressing a fabric swatch at 200°C for 45-60 seconds settles any doubt about a specific blend before committing a production run.
Why can’t you sublimate on cotton?
The failure is chemical, not technical. Sublimation uses disperse dyes that sublime into gas at roughly 200°C and bond by forming links with polyester’s hydrophobic polymer chains as they cool, becoming part of the fiber itself. Cotton is cellulose, a different polymer with hydrophilic chemistry and no receptor sites for disperse dye, so the dye gas condenses back to solid sitting loosely on the surface and washes out within the first few cycles. No temperature, paper, or press adjustment changes this, because the receptor chemistry is missing. Every successful workaround, HTV, coating spray, or DTF, works by inserting a compatible layer or replacing the dye system entirely, which is why those methods succeed where process tweaks fail.
Verdict
Sublimation printing on cotton works only through workarounds, and the data ranks them clearly: sublimation HTV for durability at 95% color after 30 washes, coating spray for cost at 85%, and DTF for production, where 160°C for 15 seconds delivers grade 4-5 fastness across 50+ washes on any fiber blend. Keep sublimation for the 60%+ polyester, light-garment work it excels at, and route cotton orders to DTF rather than fighting the chemistry; the sublimation printers lineup covers the polyester side, and a matching DTF printer covers everything else.
Sources
- Wikipedia: Dye-sublimation printing: process chemistry behind disperse dye sublimation referenced in the mechanism section.
- Wikipedia: Disperse dye: the dye class used in sublimation and its polyester affinity.
- AATCC: color fastness grading standards behind the 50+ wash benchmarks.
- Wikipedia: Cotton: cellulose fiber properties referenced in the bonding explanation.
