
Sublimation printing on wood works, but only through a polymer workaround: dye sublimation bonds exclusively to polyester and polymer-coated surfaces, so bare wood needs a poly coating, and the method that succeeds, white base plus two coats of polycrylic pressed at 385 °F for 60 seconds, is a craft process rather than a production one. This guide explains the chemistry that blocks bare-wood sublimation, compares the three coating routes that make it work, and marks the volume line where UV direct printing takes over entirely. Wood is a beautiful sublimation substrate and a terrible one to improvise on.
\n\n\n\n
Key Takeaways
\n\n\n\n- \n\n\n
- Sublimation dye bonds only to polyester and polymer surfaces, so raw wood sublimates as a faint ghost or nothing at all; every working method is a coating strategy that puts polymer between the dye and the grain. \n\n\n
- The proven craft recipe: white spray or paint base, two coats of liquid or spray polycrylic, then press at 385 °F (196 °C) for 60 seconds with parchment cover, per practitioner-documented workflows. \n\n\n
- The laminate shortcut presses a clear polyester laminate sheet to painted wood for 60 seconds first, then sublimates onto the laminate surface, trading coating labor for an extra press cycle. \n\n\n
- Direct-to-wood alternatives exist beyond sublimation: UV flatbed printing needs no coating at all and prints full photographic color directly on raw, stained, or painted wood in one pass. \n\n\n
- Production reality: sublimation-on-wood suits craft batches and personalization shops under roughly 50 pieces daily; above that, coating labor dominates and UV printing wins the math. \n\n\n
Why Bare Wood Refuses Sublimation Ink
\n\n\n\nThe chemistry is unambiguous. Sublimation ink turns to gas at press temperature and bonds molecularly with polyester chains as it cools, which is why 100% polyester fabric takes the dye permanently and why 40% polyester blends take it at 40% strength. Wood contains no polyester; cellulose fibers accept the gas passively and release it as the piece cools, leaving the faded, splotchy ghost that every crafter who skipped the coating discovers on the first press. The entire sublimation-on-wood discipline is therefore a surface-engineering exercise: build a polymer layer that the dye can bond to, keep it thin enough to press evenly, and make it transparent or white enough that the image reads through.
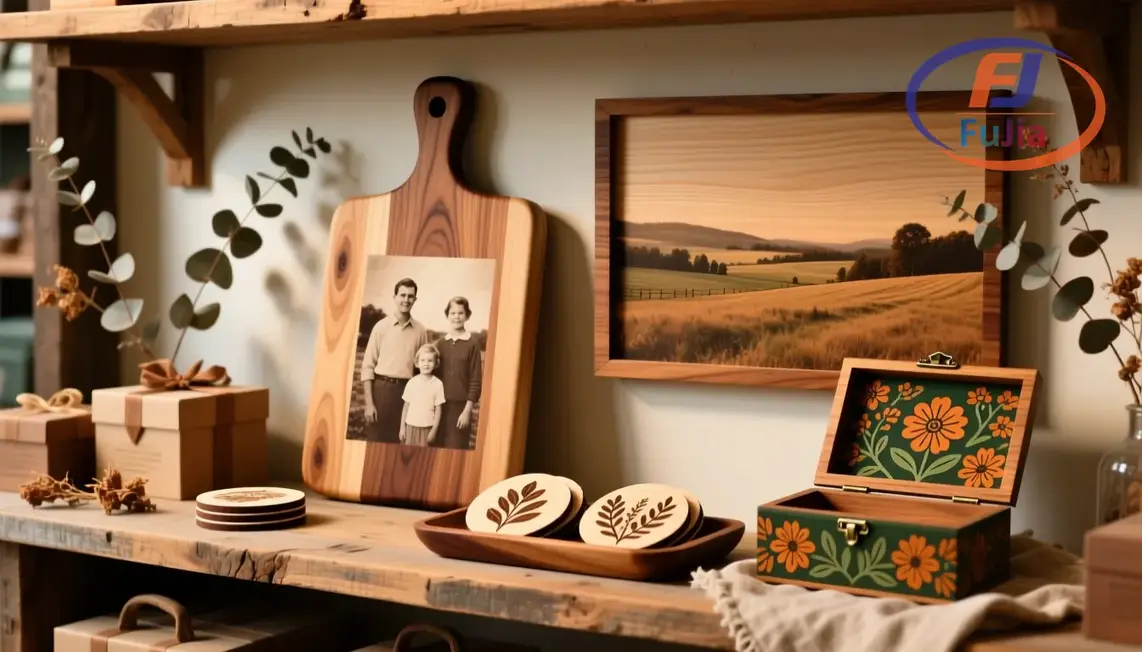
\n\n\n\nThe grain complicates what the coating solves. Softwoods like pine drink coating unevenly, leaving streaks where dye density varies; hardwoods and MDF accept thin coats consistently, which is why most sublimated wood products are birch ply, MDF panels, and hardboard coasters rather than barn-board slabs. Moisture matters too: wood with residual humidity steams under the press and bubbles the coating, so blanks should be dry-stored and pre-pressed 5-10 seconds to drive off moisture before the real transfer. The substrates that succeed consistently, coated MDF coaster blanks, birch photo panels, pre-treated wood slices, are the ones where sellers engineered the surface before the crafter ever opened the ink.
\n\n\n\nThe Three Coating Routes Compared
\n\n\n\n| Method | \nPrep | \nPress recipe | \nResult | \nBest for | \n
|---|---|---|---|---|
| Polycrylic coating | \nwhite base + 2 coats, dry 24 hr | \n385 °F, 60 s | \ndurable matte-gloss image | \ncraft production, best color | \n
| Laminate sheet | \npaint wood, press laminate 60 s | \n385 °F, 60 s over laminate | \nglossy, extra layer | \nquick batches, glossy look | \n
| Pre-coated blanks | \nnone, buy ready | \n385-400 °F, 45-60 s | \nconsistent, zero prep | \npersonalization shops | \n
The polycrylic route is the community standard because it earns the best image: the white base solves wood’s dye-transparency problem the same way white underbase works on dark garments, and the two clear polycrylic coats supply the polymer that dye actually bonds to. Practitioner testing consistently lands on 385 °F for 60 seconds with parchment paper over the transfer, and the failure modes are all prep shortcuts, single coats that leave dye-starved patches, recoating before full dry, and pressing damp wood. The laminate route compresses the prep into a first press: a clear polyester laminate sheet is pressed to painted wood for 60 seconds, then the sublimation transfer presses onto the laminate’s polyester face, and the trade is a glossier, slightly raised image against zero coating labor.
\n\n\n\nPre-coated blanks are the honest production answer for anyone selling sublimated wood rather than experimenting with it. Coated MDF and hardboard blanks from blank-supply houses run the polymer chemistry factory-consistent, press identically piece to piece, and cut the workflow to print-press-pack. A home-textiles supplier we work with illustrates the same principle from the fabric side of sublimation: matched polyester chemistry is why their Pantone-matched lines hold color across batches, and coated wood blanks import exactly that consistency into a rigid substrate. We recommend coating your own blanks only for signature sizes and finishes, and buying coated stock for everything catalog-standard.
\n\n\n\nWhen UV Printing Takes Over
\n\n\n\nThe coating workaround is honest at craft scale and dishonest at production scale, because every sublimated wood piece carries 15-30 minutes of coating and drying labor that UV printing deletes entirely. A UV flatbed prints full photographic color, with white ink for vibrancy on dark stains, directly onto raw wood, stained wood, painted wood, and sealed wood in one pass with instant LED curing, no coating, no polyester chemistry, no dry time. The varnish channel adds gloss and texture effects that sublimation cannot produce on wood at all, and per varnish economics across UV product work, those finishes command 30-50% higher per-unit pricing on premium wood pieces.
\n\n\n\nThe crossover sits near 20-50 wood pieces daily. Below that, a sublimation shop already owns the printer and press, coated blanks keep prep trivial, and wood rounds out a tumbler-and-mug catalog nicely. Above that, coating labor or blank premiums dominate unit economics, and a UV flatbed from the $5,500-8,000 tier pays for itself by deleting the entire coating stage, the same direct-to-rigid economics documented across our UV printers lineup and the promotional products applications where wood plaques and signage live. When it comes to the two-process question, sublimation wins when the product mix is already polyester-dominant. UV wins when rigid substrates are the business rather than the side dish. Most shops discover their answer within a month of tracking actual orders.
\n\n\n\n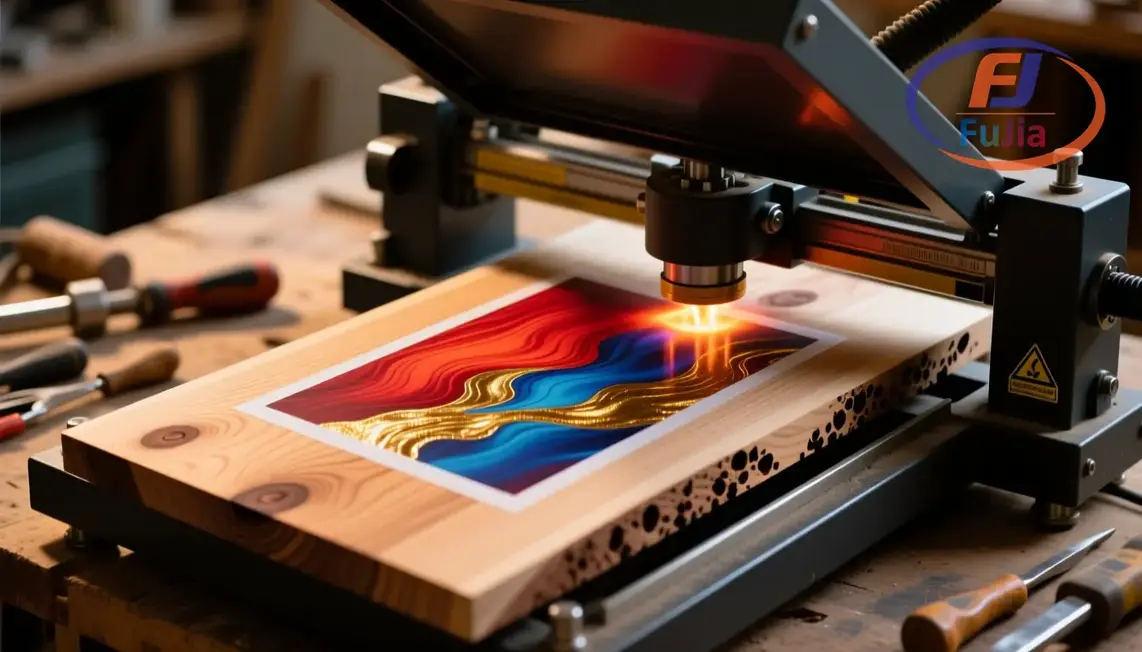
Can a sublimation printer print on wood?
\u003cp\u003eYes, with a polymer coating as the intermediary: sublimation dye bonds only to polyester, so wood must carry a polycrylic coating, a pressed laminate sheet, or a factory-applied polymer finish before the transfer presses at 385 °F for 60 seconds. Bare wood cannot accept sublimation ink and will show only a faded ghost. For uncoated wood at production volume, UV flatbed printing is the direct alternative, printing full color on raw wood with no coating stage.\u003c/p\u003e
What do you put on wood before sublimation?
\u003cp\u003eThe proven stack is a white base followed by two coats of polycrylic: white spray paint or brushed white base first, solving the dye-transparency problem, then two thin coats of liquid or spray polycrylic with full drying between coats, supplying the polymer that dye bonds to. The shortcut alternative is a clear polyester laminate sheet pressed onto painted wood for 60 seconds before the sublimation transfer. Parchment paper goes over the transfer in every method to protect the platen. Skip any layer and the result tells on itself immediately.\u003c/p\u003e
What temperature do you sublimate on wood?
\u003cp\u003e385 °F (196 °C) for 60 seconds is the practitioner-consensus recipe for polycrylic-coated and laminate-prepped wood, with pre-coated blanks running 385-400 °F for 45-60 seconds by manufacturer direction. Pre-press the blank 5-10 seconds first to drive off moisture, then press with firm pressure and parchment cover, and peel warm per the blank’s instructions. Darker or stained woods benefit from a test strip because base color shifts the transferred image the same way garment color does.\u003c/p\u003e
Can sublimation ink be used on wood without a heat press?
\u003cp\u003eA heat press is effectively required, because sublimation needs sustained, even, controlled temperature around 385-400 °F plus firm pressure for the full 45-60 second window, and household irons and ovens cannot hold that profile across a flat surface. EasyPress-class heated plates work for small blanks at craft scale with careful timing. Shops pressing more than a few wood pieces weekly need a real clamshell press, 15×15 inches minimum, which doubles for tumbler and apparel work.The iron-experiment phase costs more in ruined blanks than the press would have.\u003c/p\u003e
Verdict
\n\n\n\nSublimation printing on wood is a coating discipline: white base, two polycrylic coats or a pressed laminate, 385 °F for 60 seconds, and dry, sealed blanks, and it rewards craft batches and personalization catalogs with beautiful wood-grain-through-image pieces. At production volume the honest tool changes, and UV flatbed printing takes over with no coating, instant curing, and varnish finishes sublimation cannot touch. Master the coating recipe for signature pieces, buy coated blanks for catalog volume, and to compare UV direct printing on your own wood stock, contact Fujia Print for a sample run.
\n\n\n\nSources
\n\n\n\n- \n\n\n
- Wikipedia: Dye-sublimation printing: polyester bonding chemistry. \n\n\n
- Wikipedia: Polyurethane: polycrylic coating chemistry background. \n\n\n
- Wikipedia: Wood drying: moisture behavior under heat. \n\n\n
- AATCC: colorfastness testing standards. \n\n\n
